Featured Finishes
09.24.2026


Have you been searching for a business partner that combines the scale and technical aptitude to hard chrome plate for your complex product line?
Learn more about our diverse capabilities below:
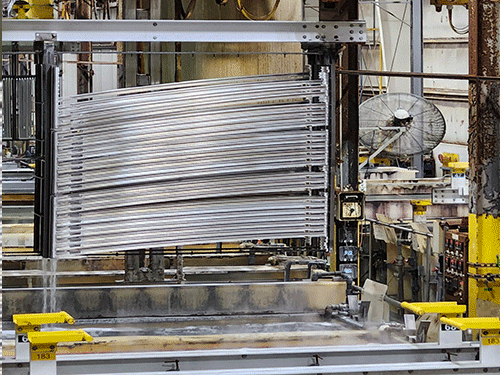
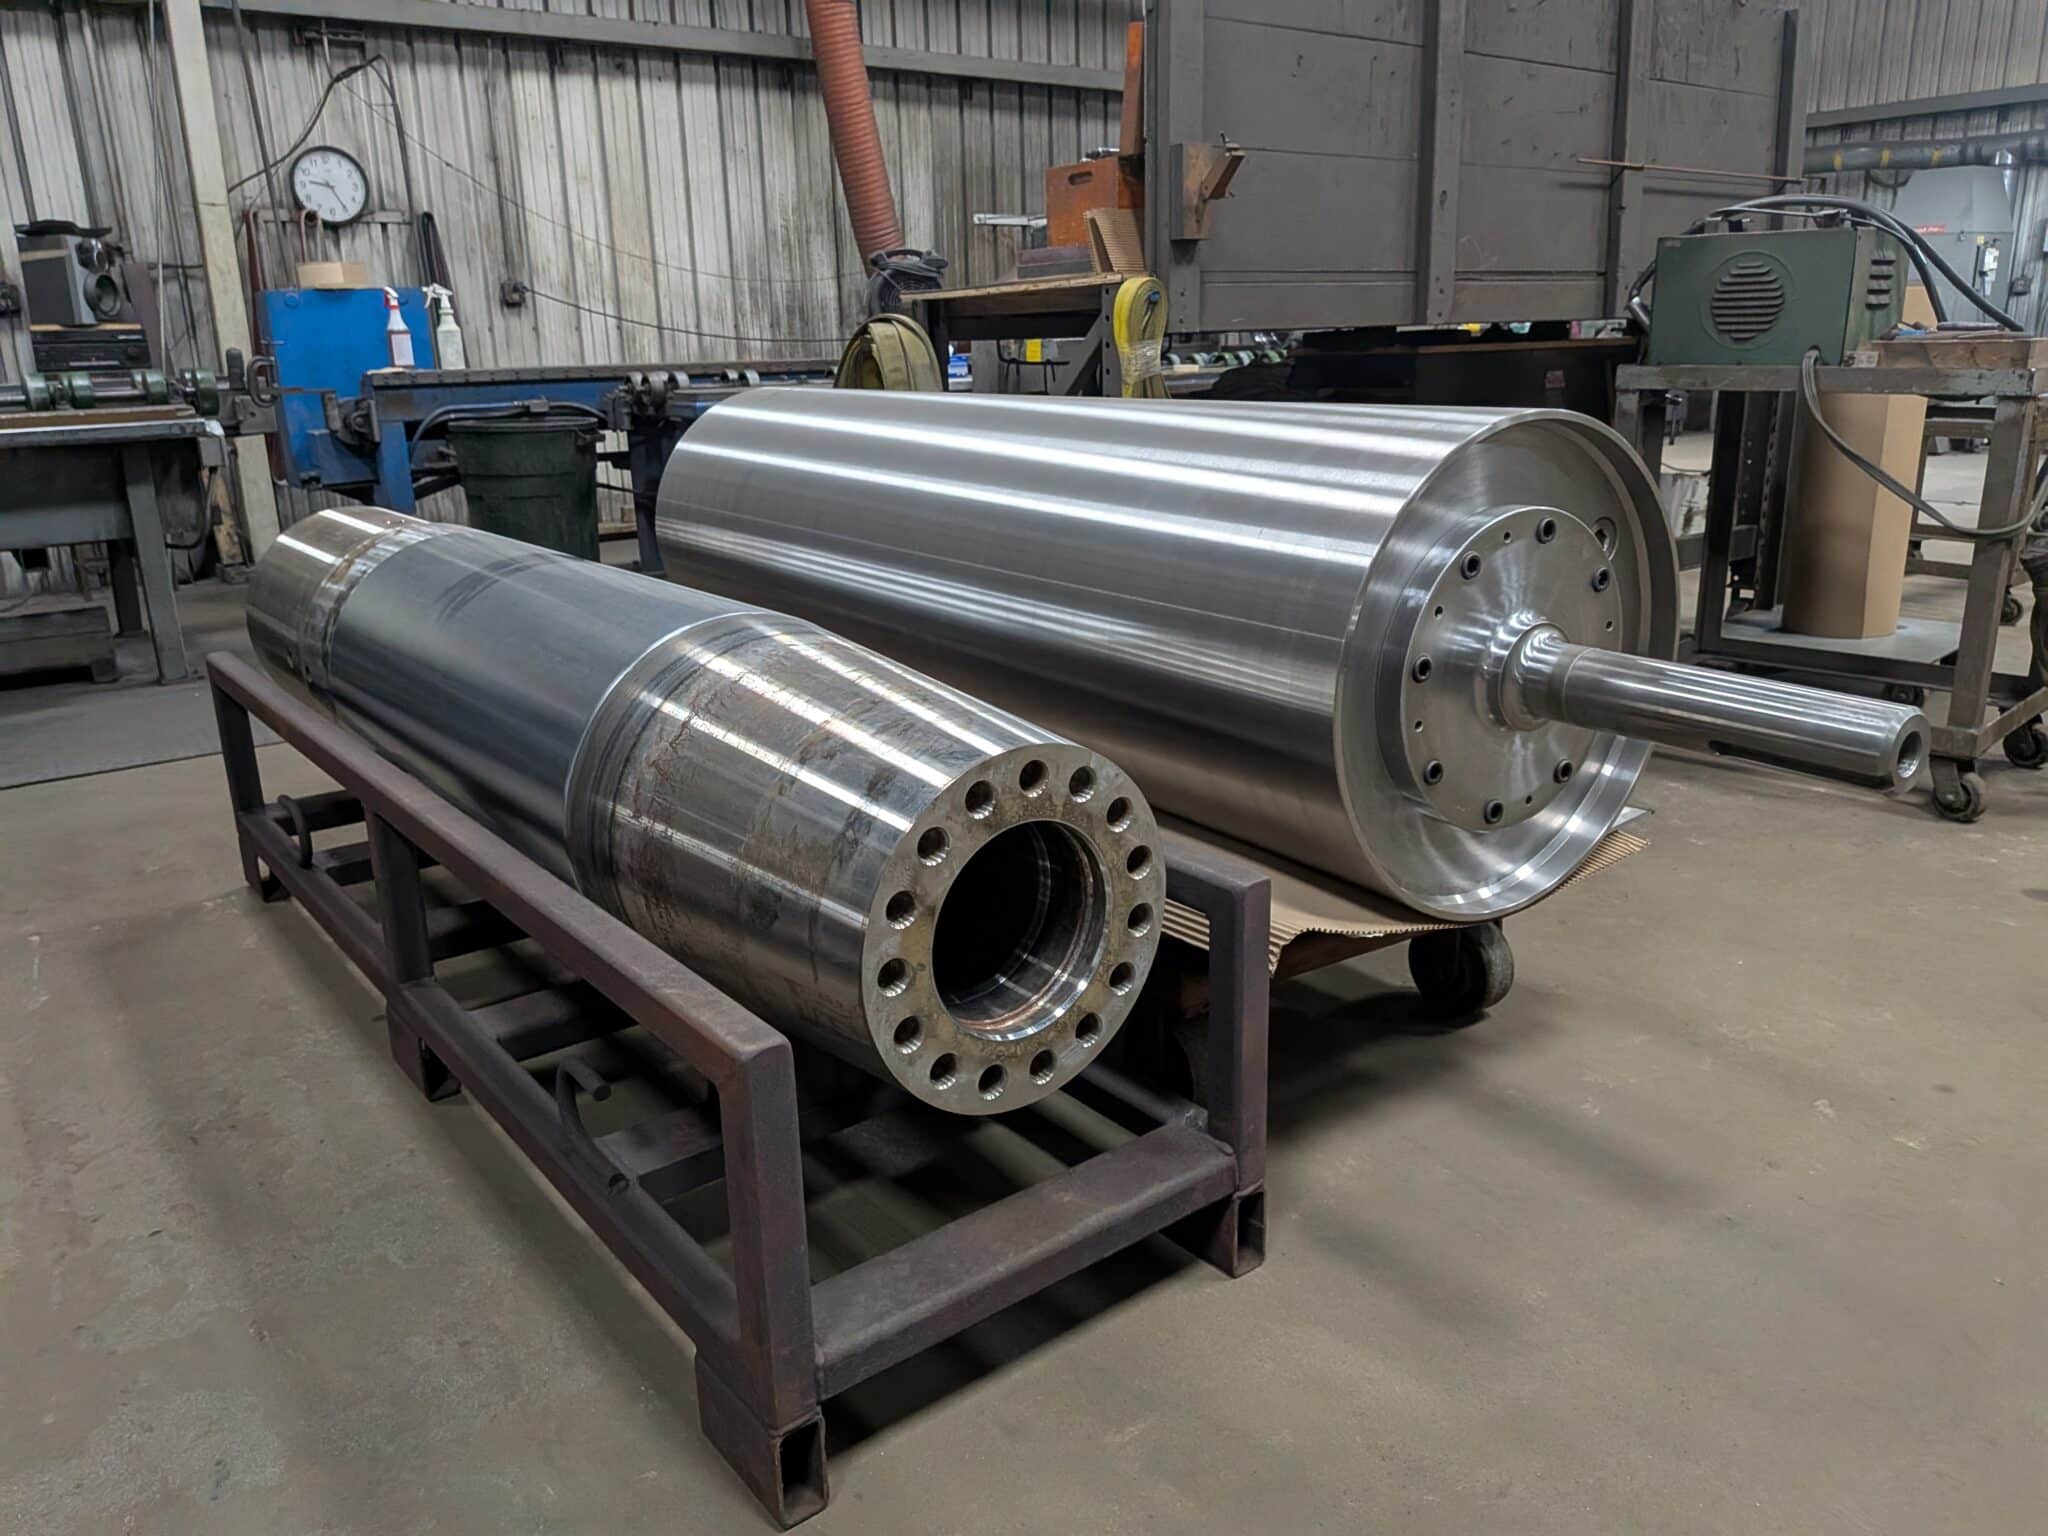
Pioneer Metal Finishing provides specialized, large-scale hard chrome plating and precision roll finishing out of our Chippewa Falls, Wisconsin facility, engineering solutions for components up to 18.5 feet in length and 10,000 lbs. The Chippewa Falls facility was explicitly designed to support dimensional extremes in both size and quantity. We specialize in the rare combination of large part geometry, critical plating tolerances, and high-capacity output that are unique in the United States.
At Pioneer Chippewa Falls, we do not leave metallurgical integrity to chance. Our approach to mitigating hydrogen embrittlement relies on absolute procedural discipline:
A: The baking parameters are dictated by the tensile strength of the base steel and the specific industry standard governing the part (such as ASTM B850 or specific Mil-Specs). Higher strength steels require longer baking durations at highly specific thermal ranges to allow the hydrogen to fully outgas.
A: We are built specifically for extreme scale. Our overhead crane network safely maneuvers components weighing up to 10,000 lbs through every stage of the workflow. For physical dimensions, our deep vertical tanks allow us to fully submerge and process components up to 18.5 feet in length and 48 inches in diameter.
A: A common point of failure for large rolls is horizontal deflection during the plating process, which leads to uneven chemical deposition. We eliminate this risk entirely by using extremely deep vertical plating tanks. This allows us to hold exceptionally tight dimensional tolerances on parts up to 18.5 feet long. Post plate, our heavy cylindrical grinding can achieve anything from a textured matte blast to an 0.3RA optically flawless mirror finish.
A: We utilize rigorous documentation and continuous oven telemetry. Furthermore, we frequently process standardized notched tensile testing specimens alongside the production lot. These specimens undergo sustained load testing to verify that delayed brittle fracture does not occur.
The modern continuous manufacturing sector is pushing equipment durability further than ever before. To succeed in this high output climate, plant reliability engineers cannot afford to treat massive component salvage as an afterthought or risk it with unequipped vendors.
Choosing the right heavy processing partner is about guaranteeing minimal line downtime and extreme risk reduction. By bringing elite vertical tank infrastructure and immense lifting capacity to our Chippewa Falls facility, Pioneer Metal Finishing ensures that your most expensive rotatory assets are restored seamlessly. If your daily challenges involve keeping paper production lines, thin film plastics extrusion, or massive steel plants running smoothly, Pioneer has the facility capacity and precise engineering to help you eliminate costly downtime.
Are you in need of project support for large part or massive volume Chrome Plating? Reach out to our Chippewa Falls Team at www.pioneermetal.com/contact.